1-10 / 1725 hits
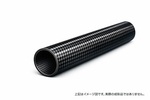
Pipe manufacturing using CFRTP (Carbon Fiber Reinforced Thermoplastics) is gaining attention as a method that combines lightweight properties, high strength, and excellent mass productivity. The method introduced here utilizes a braided CFRTP preform, combining press molding and air injection to efficiently form pipe shapes. Compared with conventional CFRP pipe manufacturing, this process significantly reduces production time and offers cost advantages. 【Overview of CFRTP Pipe Molding】 Because CFRTP uses a thermoplastic resin matrix, it can be repeatedly softened by heating and hardened by cooling. This characteristic enables fast processing with a press machine. In this method, a braided CFRTP preform is used. The process begins by wrapping the braided preform around a tube-shaped base material. Thanks to the flexibility and fiber orientation freedom unique to braided structures: Strength can be adjusted by controlling winding angles Uniform pipe structures can be formed Required rigidity can be secured efficiently 【Molding Process Flow】 The process consists of four main steps: 1. Wrapping the Braided CFRTP Preform The flexible braided preform is carefully wrapped around a base tube. By adjusting the fiber orientation during wrapping, the rigidity and strength direction of the pipe can be optimized. 2. Press Molding in a Heated Die The wrapped assembly is placed in a mold shaped to the desired pipe geometry and hot-pressed. As the thermoplastic resin softens: Fibers conform tightly to the mold surface The outer shape is precisely defined 3. Air Injection After press forming, air is injected into the interior of the pipe. This internal pressure: Stabilizes the inner diameter Ensures uniform wall thickness Improves overall rigidity and dimensional accuracy 4. Cooling and Solidification While still set in the mold, the component is cooled. As the thermoplastic resin solidifies: Final strength is established Shape accuracy is fixed A lightweight, high-rigidity CFRTP pipe is completed 【Comparison with Conventional Methods】 Carbon fiber pipes are commonly produced using CFRP (Carbon Fiber Reinforced Thermosetting Plastics). In conventional manufacturing: Prepreg is wrapped around a mandrel The assembly is cured in an autoclave While this method produces high-quality pipes, it requires long heating and curing times, limiting productivity. In contrast, CFRTP pipe molding: Utilizes thermoplastic resin properties Enables short cycle times Allows rapid press-based processing Supports continuous production for standardized sizes Higher productivity directly contributes to cost reduction. 【Application Potential of CFRTP Pipes】 CFRTP pipes offer: Lightweight construction High impact resistance Fast manufacturing speed Potential applications include: Mechanical components Sporting goods Transportation equipment requiring weight reduction The braided preform structure allows more flexible fiber orientation design than traditional CFRP pipes, enabling performance customization according to specific application needs. 【Summary】 By combining braided CFRTP preforms, press molding, and air injection, this manufacturing method enables the production of lightweight and high-strength pipes in a short time. Compared with conventional autoclave molding: Production efficiency is significantly improved Manufacturing costs can be reduced Rapid prototyping and small-lot production are feasible Although size limitations exist, this process is highly effective for components within a practical dimensional range. If you are exploring lightweight, high-strength, and cost-efficient pipe solutions, CFRTP pipe molding presents a strong alternative worth considering. 【Contact Information】 Kawamura Kikai Co., Ltd. Head Office: 2-4 Shimizu-cho, Itabashi-ku, Tokyo 【Composite Division】 Hanazono Factory: 10 Kitane, Fukaya-shi, Saitama 【Metal Press Division】 Website: https://www.kawamura-kikai.co.jp Inquiry / Quotation: https://www.kawamura-kikai.co.jp/contact/ Please mention that you saw us on “Emidas” when making your inquiry.
| Main 3 products | Automotive functional parts Truck exterior parts Industrial machinery parts |
|---|---|
| Type of manufacturing | Industrial machinery Transportation equipment |
| Recommended manufacturing category |
1:Die manufacturing - Press die - Blanking die 2:Die manufacturing - Press die - Drawing die 3:Die manufacturing - Press die - Single press die 4:Die manufacturing - Press die - Progressive die 5:Mass production - Metal press - Bending 6:Mass production - Metal press - Thickness: over 9.0 mm 7:Mass production - Metal press - Thickness: 0.2 mm - 3.2mm 8:Mass production - Metal press - Thickness: 3.2 - 9.0 mm 9:Assembly/Inspection - Assembly - Auto parts assembly 10:Assembly/Inspection - Assembly - Industrial machinery assembly |


In-house design and production of precision press die&mold. Die&mold procurement from our overseas bases is also possible with reasonable cost. Mizuho Spring Seisakusho Co., Ltd. 5-80 Urasato, Midori-ku, Nagoya shi TEL 052-624-2031 FAX 052-621-2291
| Main 3 products | Metal press and precision spring manufacturing Temporary staffing, recruitment and business consignment Precision press die manufacturing and sales |
|---|---|
| Type of manufacturing | Transportation equipment Office appliances Office automation equipment |
| Recommended manufacturing category |
1:Die manufacturing - Press die - Part processing 2:Die manufacturing - Press die - Progressive die 3:Die manufacturing - Press die - Single press die 4:Die manufacturing - Press die - 60 - 300 t 5:Parts manufacturing - Spring - Compression coil spring 6:Parts manufacturing - Spring - Piano wire (carbon wire) 7:Parts manufacturing - Spring - Formed wire spring |

Our company also performs injection molding using bio-plastics. In particular, we focus on developing and producing products using biodegradable resin “PLA (Polylactic Acid)” made from plant starch and sugars. This is a new molding solution that achieves a balance of functionality, design, and sustainability. ▪ Features and Technical Examples - Achieved thin-wall molding with 100% PLA (without blending petroleum-based resins), which was previously considered difficult. - World-first molding: wall thickness 0.65mm, flow length 135mm. - Applied long-accumulated know-how from reflector molding, etc. - Reduced resin usage through thin-wall design. - Weight reduction using MuCell® (microcellular foaming system). - Zero scrap with hot runner system. - CO₂ emission reduction by replacing petroleum-based resins. ▪ Applications and Deployment - Replacement of petroleum-based products with plant-derived materials. - SDGs-conscious novelty products to enhance corporate appeal. ◎ Consultation We handle everything from product planning, collaboration, mold manufacturing to mass production. Please feel free to contact us for injection molding with resins other than PLA. We also welcome inquiries for quotations and samples of our original products “Bio7”, “4Tiers”, and “N1”! ◎ Related Articles PLA Glass “Bio7”: https://ja.nc-net.or.jp/company/1285/product/detail/265575/ PLA Glass “4Tiers”: https://ja.nc-net.or.jp/company/1285/product/detail/265576/ PLA Glass “Foam”: https://ja.nc-net.or.jp/company/1285/product/detail/265581/ Heat-Resistant PLA Mug “N1”: https://ja.nc-net.or.jp/company/1285/product/detail/265578/ ◎ Contact Nissin Precision Machines Co., Ltd. – Head Office 〒146-0095 2-29-21 Tamagawa, Ota-ku, Tokyo, Japan TEL: 03-3758-1901 E-mail: gn_info@nissin-precision.com
| Main 3 products | Precision Progressive Press Mass-Produce Reflex Reflector Molded Products and Mol CNC Brief Form Pipe Bender |
|---|---|
| Type of manufacturing | Jigs and tools Industrial machinery Electronic parts |
| Recommended manufacturing category |
1:Die manufacturing - Press die - Progressive die 2:Die manufacturing - Press die - Drawing die 3:Mass production - Metal press - Drawing 4:Die manufacturing - Press die - Bending die 5:Die manufacturing - Press die - 60 - 300 t 6:Mass production - Metal press - Stainless steel 7:Mass production - Metal press - Iron 8:Mass production - Metal press - Aluminum 9:Mass production - Metal press - Copper 10:Die manufacturing - Plastic mold - Injection molding die |


[Machined SUS316L 3D shape, surface roughness, chemical/medical business] 【Material】 SUS316L 【Dimension】 Outer diameter φ95 【Lot】 1 to 100 pieces 【Precision】 ±0.05㎜ 【Processing method】 Machining, wire cut 【Industry/Application】 Chemical, semiconductor, medical business related 【Features】 This is a stainless steel precision item made of SUS316L that is used in the chemical and pharmaceutical industries. SUS316L clearly has inferior machinability when compared to SUS304. We chose and prepared a knife suited for SUS316L processing. As shown in the photo, the product has a round form, but through trial and error in setup and construction methods, we were able to finish it virtually entirely by machining. The slope at the top of the photo is where the liquid flows, so a severe surface roughness is required. Using optimal cutting tools and processing conditions, we are able to create a high surface roughness even when liquids flow through it. We carefully examine the blades and processing conditions used depending on the material and processing content, and strive to provide our customers with high-quality products in short delivery times. ☆Shimizu Trym Precision Inc., a manufacturer of precision parts and precision molds☆ 421-1 Shinden Nagasaki, Shimizu-ku, Shizuoka-shi, Shizuoka TEL:+8154-340-6631 FAX:+8154-340-5571 mail:eigyo@shimizutrym-pc.co.jp http://www.shimizutrym.co.jp/ We process anything from mold parts to industrial parts, precision parts, and ultra-precision parts regardless of material! by Nobita
| Main 3 products | Press mold parts Various metal/non-metal parts Semiconductor parts |
|---|---|
| Type of manufacturing | Measuring machinery Industrial machinery Electronic parts |
| Recommended manufacturing category |
1:Die manufacturing - Press die - Manufacturing 2:Die manufacturing - Press die - Blanking die 3:Designing - Jig and tool designing - Mass production jig designing 4:Development and production of prototype/Small-scale production - Jig manufacturing - Mass production jig manufacturing 5:Parts manufacturing - Other parts - Blade manufacturing 6:Development and production of prototype/Small-scale production - Sheet-metal processing - Can manufacturing 7:Development and production of prototype/Small-scale production - Machining - Handles microfabrication 8:Surface treatment - Polishing/Lapping - Mirror polishing 9:Assembly/Inspection - Assembly - Auto parts assembly 10:Designing - Jig and tool designing - General jig designing |

This is a pallet made from recycled materials of containers and packaging. We do product design and mold production. Type Size Weight Both sides 1100×1100×150 35 kg One side 1100 x 1100 x 150 34 kg, hand lift possible Both sides (light weight) 1100×1100×150 26 kg One side (light weight) 1100×1100×150 25 kg, hand lift possible Both sides (light weight) 1400 x 1100 x 140 34 kg Movable load: 1t (Dynamic load) ・ 3t (Static load) We also do sales. Please feel free to contact us for product design, mold production, manufacturing and sales of various pallets.
| Main 3 products | Automotive interior press die, dedicated machine for surface pressure tightening KP sheet, kenaf, deck, KPla sheet Recycling pallets, variable pallets, plastic floor board, pliers |
|---|---|
| Type of manufacturing | Not selected |
| Recommended manufacturing category |
1:Designing - Mold designing - General metal press die 2:Die manufacturing - Press die - Manufacturing 3:Die manufacturing - Press die - Blanking die 4:Die manufacturing - Press die - Designing 5:Development and production of prototype/Small-scale production - Prototype processing - Prototype/Small-lot molding 6:Mass production - Welding / welding - TIG welding (argon welding) 7:Development and production of prototype/Small-scale production - Jig manufacturing - General jig manufacturing |

Usage: Contact points for hand-held chargers Material: C1720-1 / 2H Plate thickness: 0.15 mm Progressive Die Minimize contact burr. Since 3 pieces are installed in parallel (using 3 pieces), the heights of the contact parts must be the same. Dimensional accuracy is required despite the complicated bending
| Main 3 products | Precision progressive die design and manufacture Precision stamping Various single-shot mold design and production |
|---|---|
| Type of manufacturing | Telecommunication equipment Electronic parts Medical equipment |
| Recommended manufacturing category |
1:Die manufacturing - Press die - Progressive die 2:Mass production - Metal press - Progressive press (35 - 80 t) 3:Mass production - Metal press - Single press (below 80 t) 4:Designing - Mold designing - General metal press die 5:Development and production of prototype/Small-scale production - Electrical discharge machine - Electric discharge machining 6:Die manufacturing - Press die - Manufacturing 7:Die manufacturing - Press die - Designing 8:Development and production of prototype/Small-scale production - Electrical discharge machine - Micro hole machining 9:Mass production - Metal press - Stainless steel 10:Mass production - Metal press - Thickness: below 0.2 mm |

ONLY ONE Processing Technology [Split Method] Splits a plate into three parts.
| Main 3 products | Welding and parts assembly Mold design and mfg Single press stamping |
|---|---|
| Type of manufacturing | Heavy electric machinery Transportation equipment Electrical component for transportation equipment |
| Recommended manufacturing category |
1:Die manufacturing - Press die - Shaving die 2:Mass production - Metal press - Transfer press (200 - 500 t) 3:Mass production - Metal press - Progressive press (80 - 200 t) 4:Mass production - Metal press - Shaving 5:Mass production - Metal press - Transfer press (80 - 200 t) 6:Designing - Mold designing - Progressive die designing (auto) 7:Designing - Mold designing - Transfer press die designing 8:Die manufacturing - Press die - Transfer press die 10:Assembly/Inspection - Inspection - Metal press |
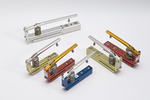
Stress-free shooting feeling We have developed a world’s smallest ultra precision stamping die handheld punch. *Visually check for punching positions is possible. *Longevity of sharpness With the smallest clearance of less than 0.005mm, outstanding sharpness lasts for a long time. In addition, It can be used on metallic foils that are difficult to process with ordinary hand punches without burrs, deformation, and appearance of foreign substances. *Light weight and compact size It is designed to be light weight and compact which can easily handled by females. It is possible to punch with applying less force, resulting in the increase of operational efficiency! Shock resistant design The jamming doesn’t appear even if it is dropped unintentionally. *Less foreign substances intervention will occur due to use of this product. We have 4 kinds of standard sizes! We also have 7 different colors, allowing you to apply them to recognize different manufacturing processes and shapes. It’s possible to add convenient options. Please send us documents with required measurements. For more details, please check our web site.
| Main 3 products | Design and production of ultra precision jigs Design and production of precision stamping dies, and production of precision stamping parts Production of precision machine parts and precision stamping die parts |
|---|---|
| Type of manufacturing | Not selected Jigs and tools Industrial machinery |
| Recommended manufacturing category |
1:Die manufacturing - Press die - Blanking die 2:Parts manufacturing - Other parts - Blade manufacturing 3:Development and production of prototype/Small-scale production - Jig manufacturing - General jig manufacturing 4:Mass production - Metal press - Combined press-joining 5:Product manufacturing - Medical equipment manufacturing - Medical equipment manufacturing 6:Development and production of prototype/Small-scale production - Prototype processing - Small-size prototype manufacturing 7:Mass production - Grinding processing - Plane grinding 8:Surface treatment - Polishing/Lapping - Mirror polishing 9:Designing - Jig and tool designing - General jig designing 10:Die manufacturing - Cutting dies - Thomson punch |

This component is a spring for a spacer. Component size: 4mm Plate thickness: 0.2mm Processing method: Stainless steel is processed using a 45-ton press.
| Main 3 products | Caulking press Flat spring parts Press/die manufacturing |
|---|---|
| Type of manufacturing | Home electrical appliances Telecommunication equipment Electronic parts |
| Recommended manufacturing category |
1:Die manufacturing - Press die - Progressive die 2:Mass production - Metal press - Thickness: 0.2 mm - 3.2mm 3:Mass production - Metal press - Combined press-joining 4:Mass production - Metal press - Thickness: below 0.2 mm 5:Mass production - Metal press - Progressive press (35 - 80 t) 6:Mass production - Metal press - Copper 7:Mass production - Metal press - Phosphor bronze 8:Mass production - Metal press - Brass 9:Mass production - Metal press - Stainless steel 10:Designing - Mold designing - General metal press die |

NAOYA HIDA & Co.は、飛田直哉氏が手がける時計ブランドです。 熟練職人による手作業と最新鋭工作機械による加工を組み合わせた現代のヴィンテージ ウォッチ 協栄プリント技研株式会社では、独自の技術で、デザインを忠実に切削加工をした 時針、分針、秒針を提供しております。
| Main 3 products | Precision press dies [Design, manufacture and sales] Micro-manufactured parts [Manufacture and sales] |
|---|---|
| Type of manufacturing | Jigs and tools Telecommunication equipment Electronic parts |
| Recommended manufacturing category |
1:Die manufacturing - Press die - Blanking die 3:Development and production of prototype/Small-scale production - Prototype processing - Simple mold, prototype mold 4:Die manufacturing - Cutting dies - Cutting blade cutting die 5:Development and production of prototype/Small-scale production - Machining - Machining/Handles small-scale production (order from 1 piece) 6:Die manufacturing - Rubber mold - Light electrical/earthing rubber 7:Die manufacturing - Press die - Fine blanking die |
1-10 / 1725 hits